
 Español
 عربى

Industry News
Home / News / Industry News / Debinding and Sintering Furnace Guide: Process, Selection & Best Practices
Debinding and Sintering Furnace Guide: Process, Selection & Best Practices
Date:Sep 08, 2026
The green part looks flawless: sharp edges, smooth surfaces, dimensions straight from the mould. Then it runs through a debinding and sintering furnace, and 24 hours later you find a hairline crack, a sagging corner, or a density just below specification. In almost every case, the culprit is the thermal process, not the powder.
Bottom line: a debinding and sintering furnace is only as reliable as its temperature uniformity, atmosphere control, and binder-waste management. Get those three right and the furnace will produce dense, dimensionally accurate parts repeatably. Get them wrong and no downstream inspection step can save the batch.
In metal injection moulding (MIM), powder injection moulding (PIM), ceramics, and binder-based additive manufacturing, the furnace turns a powder-binder compact into a dense component. The debinding phase removes the organic binder that gave the powder its shape; the sintering phase densifies the remaining powder through atomic diffusion at temperatures typically between 60% and 85% of the material's melting point. Because both phases share one thermal system, furnace selection has an outsized effect on part quality, cycle cost, and throughput.
Content
How a Debinding and Sintering Furnace Works
A complete cycle runs through three stages, each with different furnace demands.
Binder removal
Thermal debinding starts with a slow ramp — often 1 to 5 °C/min — into a hold window of roughly 200 to 600 °C. The binder melts, wicks to the surface, and evaporates or decomposes. That vapour must be continuously swept away by carrier gas or collected in a condensate trap. Ramp too fast and internal vapour pressure blisters or cracks the part; leave the vapour in place and it re-deposits as soot or carbon residue.
Sintering
Once most of the binder has left the part, the furnace switches to a sintering atmosphere — nitrogen, argon, hydrogen, or vacuum — and ramps to the target temperature. Powder particles fuse at their contact necks, pores shrink, and the component densifies. Linear shrinkage of 12 to 20% is normal, so radial temperature uniformity across the load is critical; a cold corner produces a low-density edge and distorted tolerances.
Cooling
Controlled cooling prevents warping and, for alloyed materials, sets the final grain structure. That is why the furnace needs programmable multi-segment control rather than a simple thermostat.
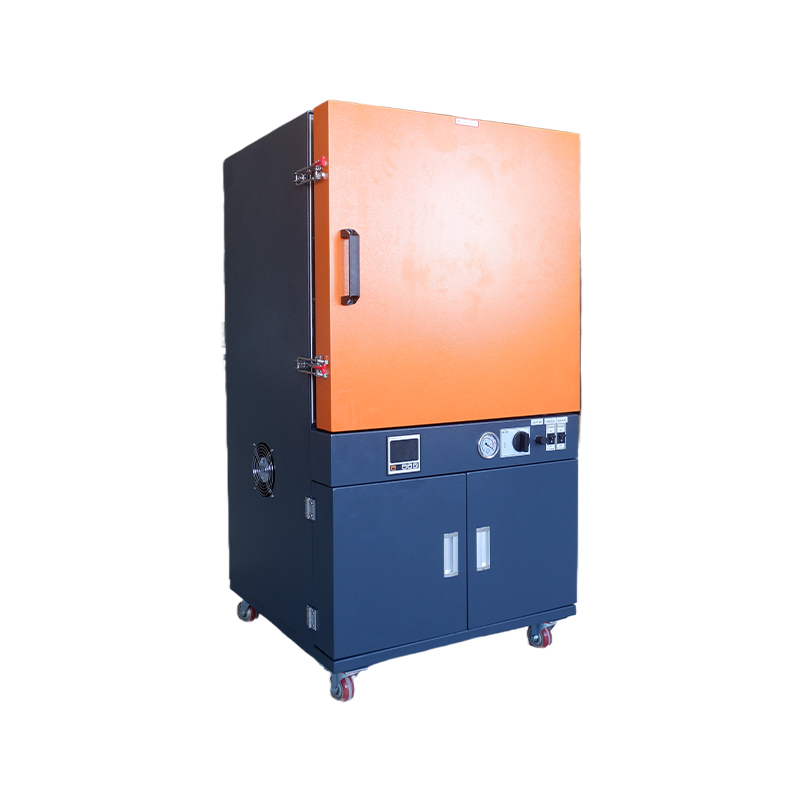
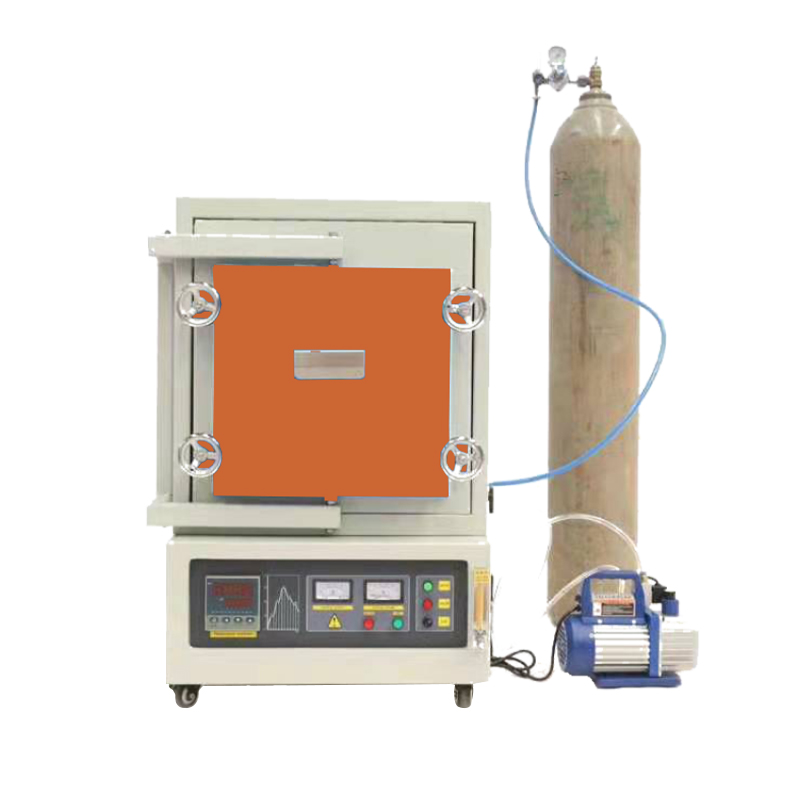 Vacuum Atmosphere Furnace with Timer for Multi-Program SinteringThis furnace supports programmable multi-segment control and a vacuum purge before inert gas backfill, making it suitable for oxidation-sensitive materials like titanium alloys while running multiple sinter programs in one unit.View Product →
For oxidation-sensitive materials such as titanium alloys, a vacuum purge before backfilling with inert gas keeps the atmosphere clean from the start of the cycle. A vacuum-atmosphere furnace with a timer function simplifies this sequence and is a practical fit when one unit must run multiple sinter programs.
Three Debinding Routes, One Quality Target
The debinding route is determined by the binder system, not the furnace. The comparison below summarises the three mainstream approaches used before or inside the sintering furnace.
Thermal-only debinding has the widest material compatibility and needs no auxiliary equipment, making it the default for laboratory development and small production runs. Catalytic debinding is faster for polyacetal binders but adds acid vapour handling. Solvent debinding shortens the later thermal step but adds storage, flammability, and disposal costs.
Hidden Metrics That Decide Part Quality
Datasheets emphasise maximum temperature and chamber volume, but three less-publicised specifications cause most field problems.
- Temperature uniformity. A ±10 °C spread across the hot zone means parts on one shelf over-densify while parts on the other stay porous. Look for a uniformity specification at your actual sintering temperature, not just at maximum temperature.
- Low-temperature ramp control. Debinding happens below 600 °C, where a furnace that overshoots creates blisters. A control loop with predictable low-power modulation matters more than a high maximum rating.
- Binder residue management. Hydrocarbons that are not swept out condense on cooler walls and can re-deposit on parts as carbon. Good furnace design includes a heated outlet, condensate collection, or an afterburner.
Sintering temperature is the first number to define in any furnace specification. Typical windows for commonly processed materials are shown below.
1350 °C
316L SS
1330 °C
17-4PH
1240 °C
Ti-6Al-4V
1500 °C
ZrO2
1600 °C
Al2O3
1450 °C
WC-Co
Approximate sintering temperature midpoints for common PIM and powder-metallurgy materials.
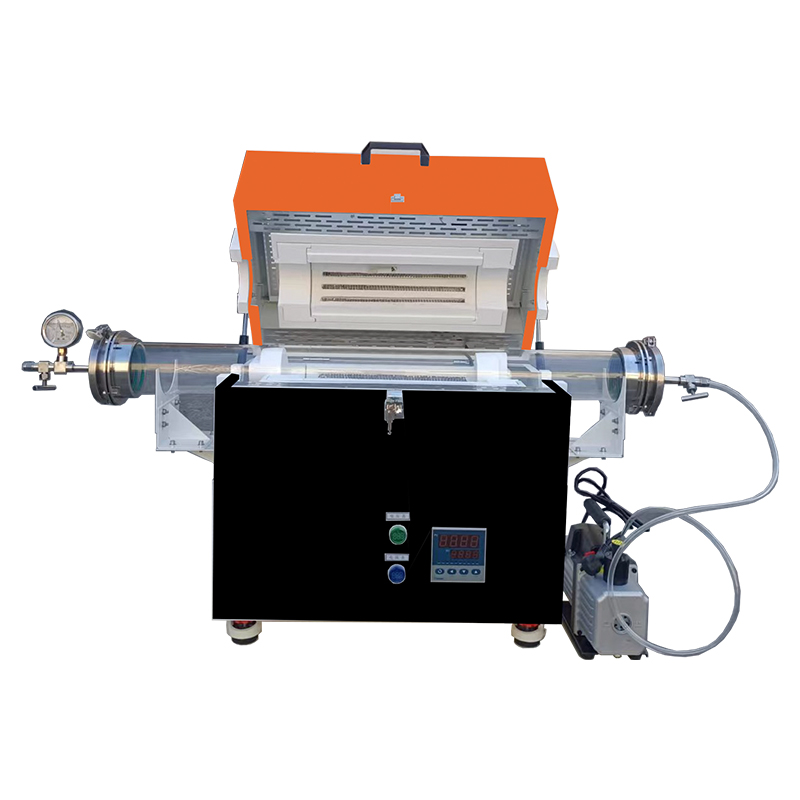 Antioxidant Vacuum Tube Furnace with 1200–1700°C OptionsOffering multiple temperature ranges up to 1700°C, this compact tube furnace enables process development for powder metallurgy and PIM materials, with easy purging and precise atmosphere control in a small footprint.View Product →
For process development, a tube furnace with multiple temperature options lets you refine the cycle in a compact, easily purged footprint before moving to a full-scale production unit.
Where These Furnaces Earn Their Keep
Debinding and sintering furnaces support a broad industrial base. The chart below shows a representative distribution of demand across typical end-use sectors.
Automotive — 25%
Medical and dental — 20%
Electronics and semiconductors — 18%
Aerospace — 15%
Industrial tooling — 12%
Consumer and other — 10%
Automotive remains the largest consumer because MIM produces thousands of small, complex parts at tolerances that would require extensive machining if made from bar stock. Medical and dental applications value the same complexity in surgical instruments, bone screws, and orthodontic brackets. Electronics relies on the clean, tightly controlled atmospheres for ceramic and metal packages, while aerospace uses the process for near-net-shape parts in demanding alloys.
A Practical Furnace Selection Guide
Start with the part and material system, then work through five decisions in order. Each one changes the specification of the furnace you should buy.
1. Define maximum temperature
Stainless steels need about 1350 °C; zirconia and alumina need 1500–1700 °C. Choose one model above your current requirement if you expect material changes.
2. Choose the atmosphere
Nitrogen suits many stainless grades; hydrogen or vacuum is required for titanium and reactive alloys. Confirm that the seals and gas train match the atmosphere you plan to use.
3. Match the hot zone to the load
Uniformity over the occupied volume matters more than total chamber size. Check whether heating elements cover every face and how the gas is circulated.
4. Plan for binder exhaust
A condensate trap, heated outlet, or afterburner prevents binder by-products from fouling the furnace. Ask for the supplier's documented cleaning procedure before you sign.
5. Estimate total cost of use
Energy, inert-gas consumption, heating-element replacement, and maintenance labour usually exceed the purchase price over a five-year period.
For material systems that sinter at or below 1300 °C, a box-type resistance furnace gives a robust balance of hot-zone volume, temperature performance, and cost for many MIM and ceramic workloads.
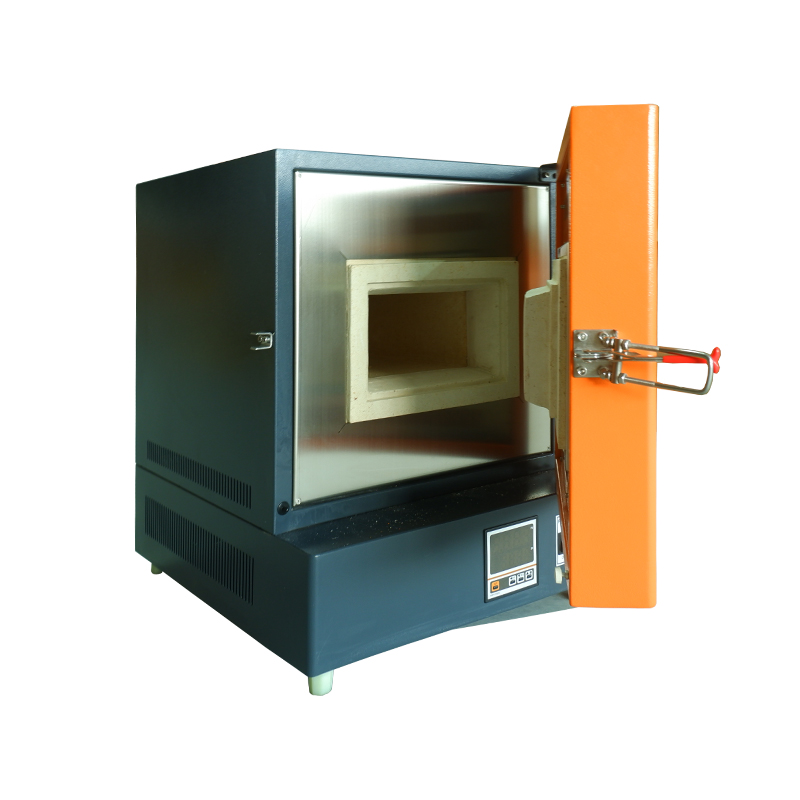 Stable-Performance Box-Type Resistance Furnace for 1000–1300°CDesigned for sintering below 1300°C, this box furnace balances hot-zone volume, temperature stability, and cost for MIM and ceramic workloads, with accurate control suited for routine heat treatment applications.View Product →
Above 1300 °C, or under a controlled atmosphere, the sealing system and gas purity become the defining features of the furnace you choose.
Maintenance and Compliance Considerations
Debinding creates the messiest operating environment a furnace will ever see. Organic vapours condense, polymerise, and gradually build up in the exhaust path. A workable maintenance plan includes three routines.
- Inspect the exhaust path. Check the condensate trap and outlet line after every debinding-heavy cycle, and clean them before the restriction raises internal pressure.
- Validate the thermal profile. Run a temperature-uniformity survey at your actual sintering setpoint every quarter, or after any heating-element change. Thermocouples drift; the parts always notice.
- Check the gas train. For inert or combustible atmospheres, verify flow rates, purge interlocks, and leak integrity before each production campaign.
Compliance is equally important. If the binder system releases flammable vapours, the furnace's electricals and ventilation must meet local explosion-protection requirements. Depending on your market, ISO 9001 quality documentation, CE marking, or pressure-vessel certification may also apply. It is worth tracking industry news on furnace safety and equipment regulation before investing in a long-lived asset.
A debinding and sintering furnace is a long-term investment in process capability, not a commodity oven. The supplier's understanding of thermal processing matters as much as the hardware: a manufacturer that builds its own furnace range, tests every unit, and supports custom configurations will save you more downtime than any price difference. That is the standard Shanghai Dengsheng applies to every high-temperature furnace it ships, and it is the right standard to hold any supplier to when you compare quotations.
Send Message
Recommended Products
Products provided by famous enterprises are deeply trusted by users.
- CONTACT
-
- No. 119, Qingliang Avenue, Yaozhuang Town, Zhejiang, China.
- [email protected] ( Email )
- +86-13671719019 ( Phone )
- +86-021-57440136 ( Tel )
- PRODUCT
-
- Drying Oven Series
- Vacuum Box Series
- Explosion-proof Series
- High-temperature Furnace Series
- Incubator Series
- Test Chamber Series
- Other Series
- Forced Air Drying Oven
- Resistance Furnace
- Vacuum Tube Furnace
- Mold Incubator
- Vacuum Atmosphere Furnace
- Biochemical Incubator
- Carbon Dioxide Incubator
- Explosion-Proof Vacuum Drying Oven
- High and Low Temperature Test Chamber
- MOBILE
Copyright ©
Shanghai Dengsheng Instrument Manufacturing Co., Ltd.
All Rights Reserved. Laboratory Equipment Manufacturers

 Back to Top
